Industrial Steam • Fluid Control • Heat Transfer • Flow Measurement
Nairobi, Kenya
Industrial Steam • Fluid Control • Heat Transfer • Flow Measurement
Nairobi, Kenya
Industrial Steam • Fluid Control • Heat Transfer • Flow Measurement
Nairobi, Kenya

Engineering Solutions
Practical Steam and Process Solutions for Industry
Peerless Engineering provides engineered products and technical support for steam, condensate, heat-transfer and process-control systems. We help customers develop reliable solutions that improve process control, reduce energy losses, enhance plant safety and deliver long-term operational value.
Our Approach
More Than Individual Components
We work with customers to understand operating conditions, identify performance challenges and select equipment suited to the required pressure, temperature, flow rate, process duty and installation environment.
Solution 01
Steam Pressure Management
Stable and Reliable Steam Pressure for Every Process
Industrial steam systems often operate at a higher pressure than individual processes require. Without proper pressure control, plants may experience unstable temperatures, inconsistent production, excessive steam consumption, equipment wear and safety concerns.
Peerless Engineering supplies steam pressure-management solutions designed to deliver stable downstream pressure while responding effectively to changes in process demand.
Our solutions may include
- Direct-acting pressure-reducing valves
- Pilot-operated pressure-reducing valves
- Pressure control valves
- Steam separators and strainers
- Safety valves and pressure gauges
- Isolation valves and pipeline ancillaries
- Complete pressure-reducing stations
Typical applications
Benefits
- Stable process temperatures
- Improved production consistency
- Reduced risk of equipment damage
- Better steam-system efficiency
- Improved control at varying process loads
- Safer and more reliable plant operation

Solution 02
Boiler Efficiency Solutions
Improve Boiler Performance and Reduce Energy Losses
The boiler house is at the centre of an industrial steam system. Poor boiler control, inadequate monitoring, heat losses, poor condensate return and inefficient blowdown practices can significantly increase fuel, water and chemical-treatment costs.
Peerless Engineering provides boiler controls, instrumentation and supporting equipment designed to help customers operate their boilers more safely, efficiently and consistently.
Our solutions may include
- Boiler level controls
- Level probes and controllers
- Conductivity and blowdown controls
- Feedwater control systems
- Steam-flow measurement
- Pressure and temperature instrumentation
- Boiler-house valves and ancillaries
- Flash-steam and heat-recovery equipment
- Condensate-return solutions
Typical challenges we address
Benefits
- Improved boiler operating efficiency
- Reduced fuel and water consumption
- Better steam-generation control
- Improved visibility of boiler performance
- Lower chemical-treatment requirements
- Improved boiler safety and reliability
- Reduced operating costs
Solution 03
Heat Transfer Solutions
Efficient Heat Transfer for Industrial Processes
Reliable heat transfer is essential for heating water, air, product and process fluids. An incorrectly sized or poorly controlled heat exchanger can result in long heating times, unstable temperatures, excessive steam consumption and reduced production capacity.
We support customers in selecting heat-transfer equipment based on the required process duty, steam pressure, inlet and outlet temperatures, flow rates, material compatibility and available installation space.
Our solutions may include
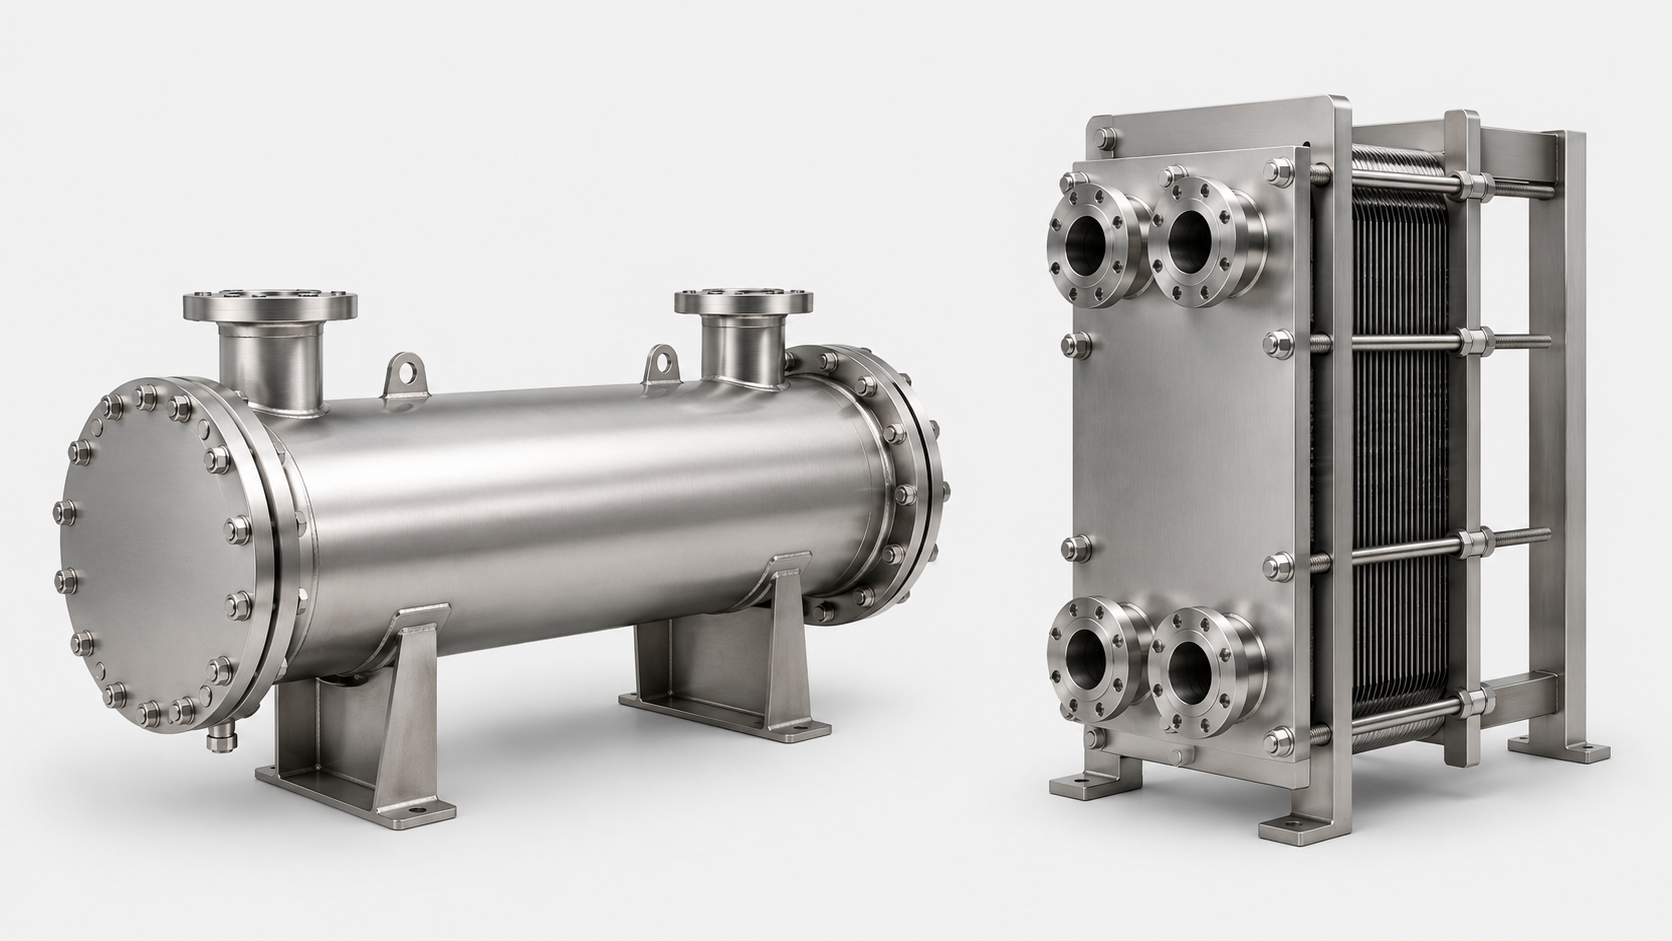
- Shell-and-tube heat exchangers
- Plate heat exchangers
- Steam-to-water heating systems
- Steam-to-air heating coils
- Calorifiers
- Process-heating packages
- Temperature-control valves
- Condensate-drainage equipment
- Steam traps and associated ancillaries
Typical applications
Benefits
- Faster and more consistent heating
- Accurate temperature control
- Reduced steam consumption
- Compact and efficient equipment selection
- Improved process productivity
- Reliable condensate drainage
- Reduced risk of waterlogging
Solution 04
Condensate Recovery Solutions
Recover Valuable Heat, Water and Treatment Chemicals
Condensate is a valuable source of hot, treated water. Discharging it to drain wastes energy, water and chemicals that can often be recovered and returned to the boiler house.
We provide condensate-recovery solutions for both gravity-return and pumped-return systems, addressing common problems such as condensate backpressure, waterlogging, steam-trap failure, low-level equipment and inadequate return-line capacity.
Our solutions may include
- Mechanical condensate pumps
- Pump-trap combinations
- Electric condensate-return units
- Steam traps
- Flash vessels
- Condensate receivers
- Check valves and isolation valves
- Sight glasses and monitoring equipment
- Flash-steam heat-recovery systems
Benefits
- Reduced boiler fuel consumption
- Lower water and chemical-treatment costs
- Increased boiler feedwater temperature
- Improved heat-transfer performance
- Reduced waterlogging and production delays
- Lower wastewater discharge
- Reduced environmental impact

Solution 05
Industrial Pipeline Solutions
Reliable Components for Steam, Water, Air and Process Pipelines
Industrial pipeline systems require properly selected valves and ancillaries to control flow, remove contaminants, isolate equipment and protect downstream processes.
Peerless Engineering supplies industrial pipeline components selected according to the process medium, pressure, temperature, pipe size, connection type, material requirements and operating environment.
Our product range may include
- Bellows-sealed isolation valves
- Globe, gate, ball and butterfly valves
- Check valves
- Strainers
- Steam separators
- Sight glasses
- Air vents and vacuum breakers
- Safety valves
- Flexible connectors
- Pressure and temperature instrumentation
- Steam traps and condensate equipment
Benefits
- Improved system reliability
- Reduced leakage and maintenance
- Better protection of control equipment
- Easier equipment isolation
- Improved steam quality
- Reduced contamination and pipeline damage
- Safer plant operation


Solution 06
Process Control Solutions
Accurate Control of Pressure, Temperature, Flow and Level
Industrial processes depend on accurate and repeatable control. Poorly selected valves, actuators or controllers can cause process instability, product-quality variations, excessive energy consumption and premature equipment failure.
Peerless Engineering provides process-control products and technical support for steam, water, air and compatible industrial fluids.
Our solutions may include
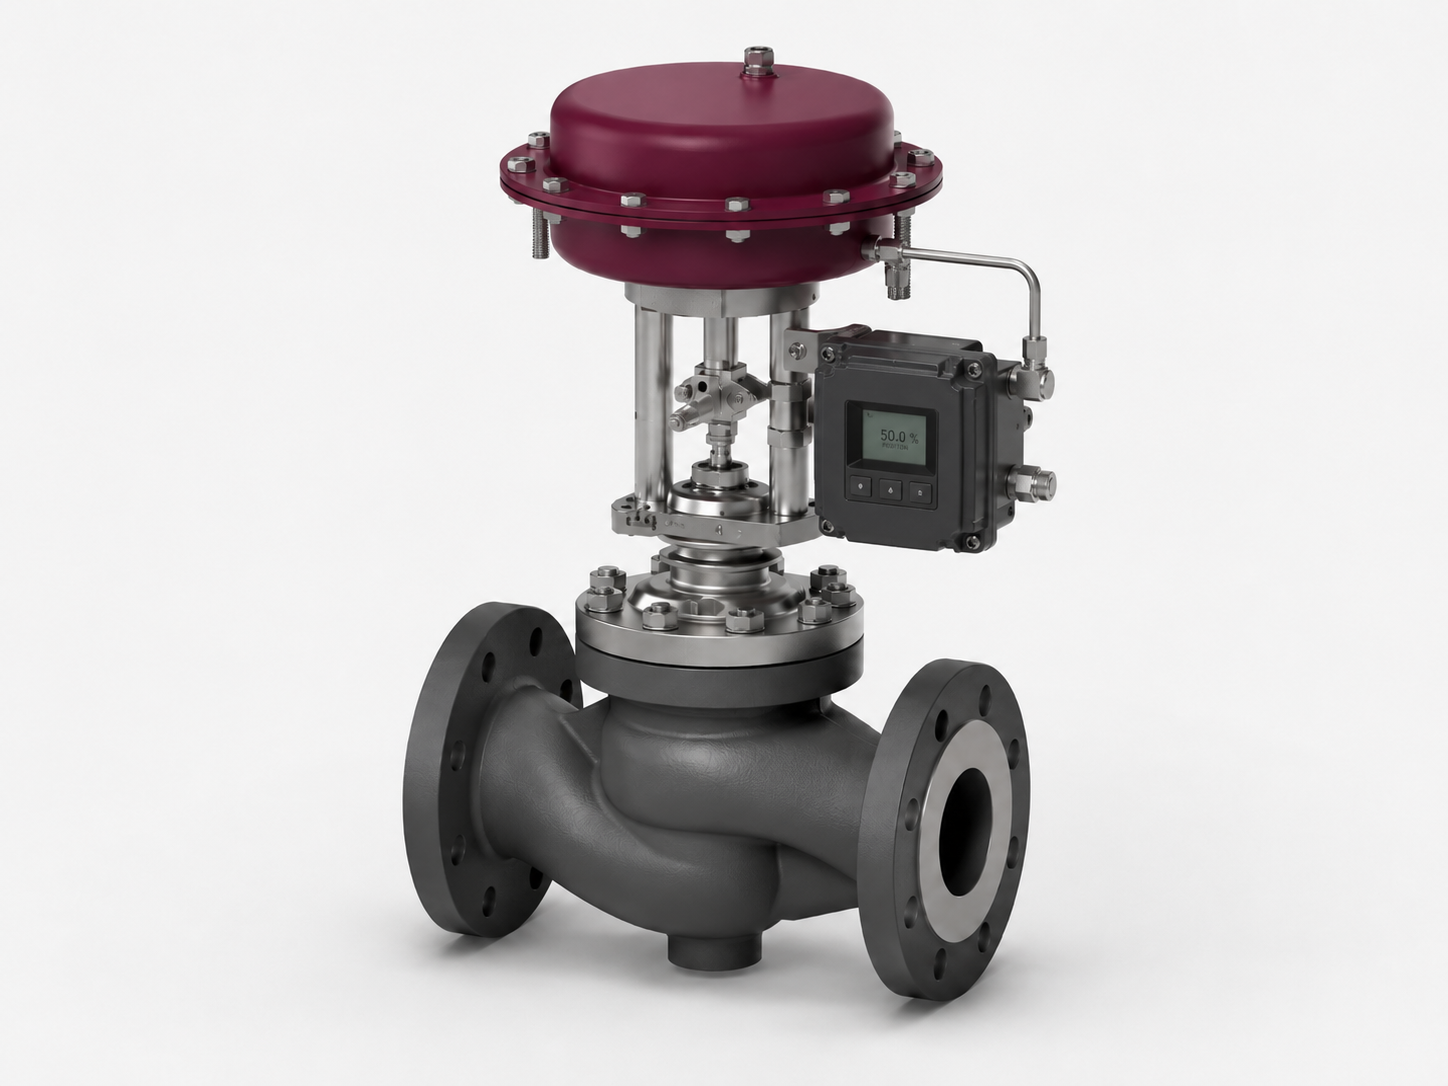
- Pneumatic and electric control valves
- Valve actuators
- Smart and conventional positioners
- Temperature controllers
- Pressure controllers
- Level-control systems
- Flow-control solutions
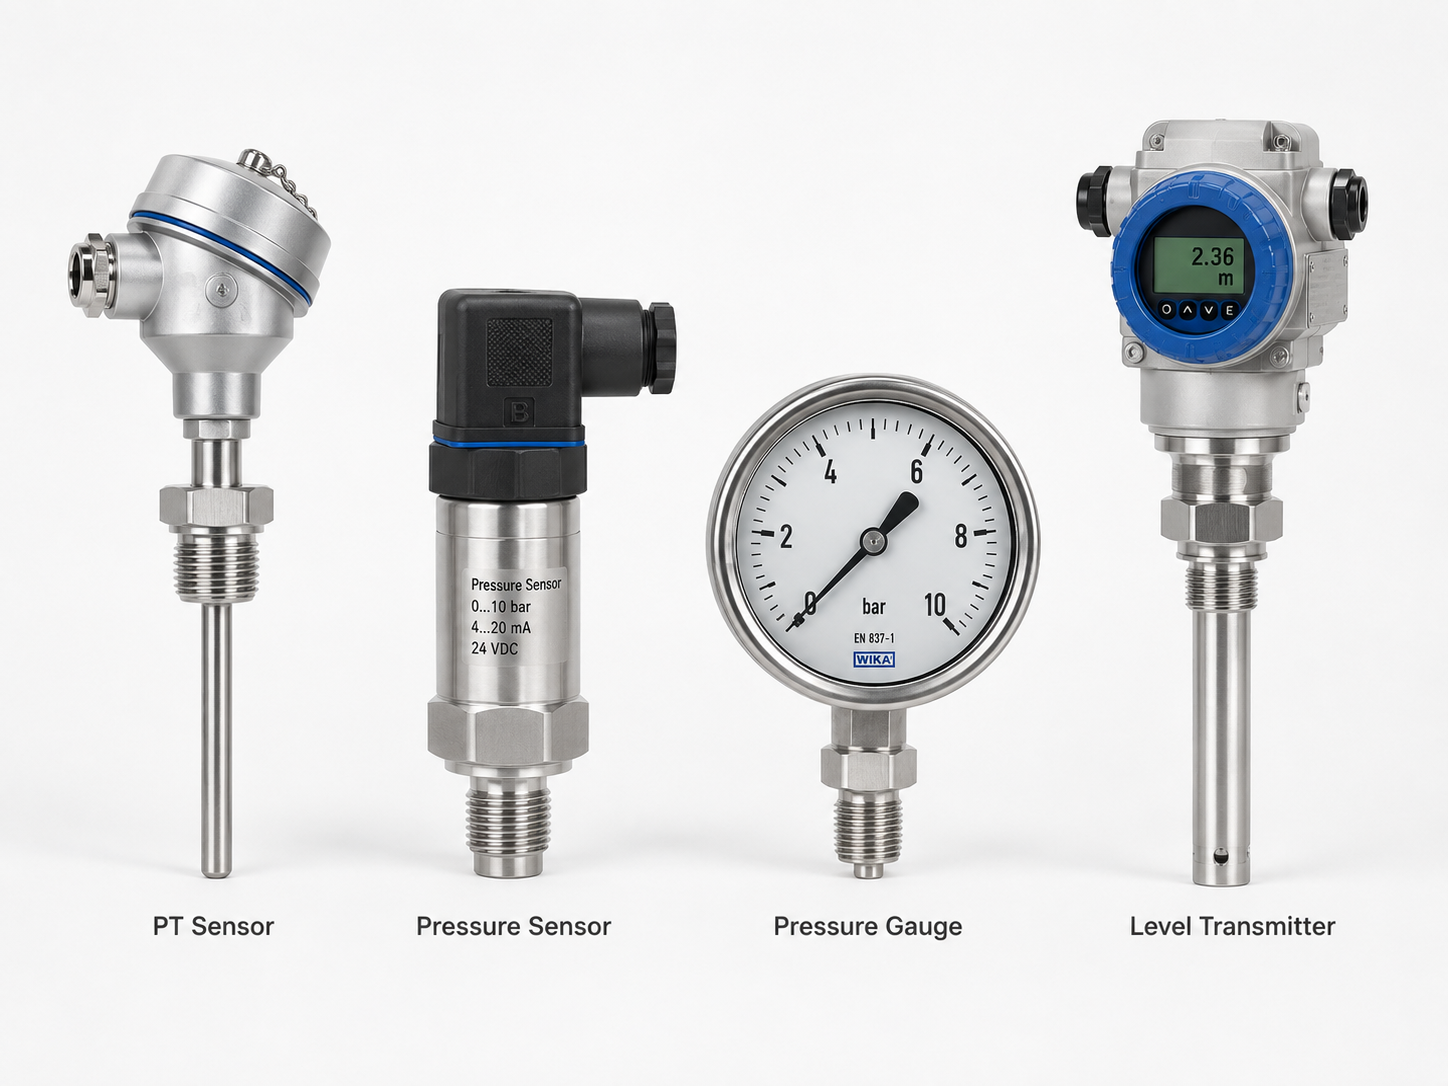
- Pressure and temperature sensors
- Control panels and associated accessories
Typical applications
Benefits
- More stable process conditions
- Improved product consistency
- Reduced energy consumption
- Better response to changing loads
- Improved equipment protection
- Easier integration with plant automation
- Reduced operator intervention
Need Help Selecting the Right Solution?
Send us your operating conditions, existing equipment details or project requirements. Our team will review the information and respond with appropriate technical and commercial guidance.
Sales: sales@peerless-engineering.com · WhatsApp: +254 799 655 007